

Skived and Roller-Burnished Tube (SRB)
Skived & Roller-Burnished Tube (SRB Tube)
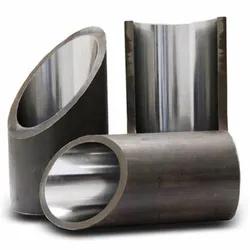
Precision hydraulic cylinder tube with a mirror-finish, work-hardened bore — delivered ready to assemble, no honing required.
1. Product Overview
Skived and Roller-Burnished (SRB) tube is a ready-to-use cylinder barrel manufactured from cold-drawn seamless or welded (DOM) mother tube. In a single pass, a combined tool first skives the bore to near-final size, then roller-burnishes it to exact H8/H9 tolerance with a smooth, cold-worked surface.
The result: tighter and more consistent bore geometry, a harder running surface for longer seal life, and shorter lead times than conventional multi-pass honing.
| Key Figure | Value |
|---|---|
| Finished ID | 20–500 mm (larger on request) |
| Wall thickness | 2–40 mm (up to 60 mm on request) |
| Length | Up to 12,000 mm (cut-to-length available) |
| Bore tolerance | H8 / H9 |
| Bore roughness | Ra 0.2–0.4 μm (≈ 8–16 μin) |
| Standard materials | E355 (St52), E235 (St37), 1026 DOM |
2. How It's Made — The SRB Process
| Step | Description |
|---|---|
| 1. Mother tube | Cold-drawn seamless tube (EN 10305-1/-4) or drawn-over-mandrel welded tube (EN 10305-2 / ASTM A513 Type 5), supplied with machining allowance on the bore |
| 2. Skiving | Carbide knives machine the ID to near-final size, correcting roundness and removing any surface defects |
| 3. Roller burnishing | Hardened rollers cold-roll the bore to final dimension, plastically smoothing and compressing the surface layer |
| 4. Finishing | Cleaning → 100% dimensional and roughness inspection → anti-rust oil → end capping |
3. Technical Specifications
3.1 Dimensions & Tolerances
| Parameter | Specification |
|---|---|
| Inner diameter (finished) | 20–500 mm |
| Wall thickness | 2–40 mm (±10% or by agreement) |
| ID tolerance | H8 (standard) or H9 — e.g., Ø100 H8 = +0.054 / 0 |
| ID surface roughness | Ra 0.2–0.4 μm |
| OD tolerance | Per mother-tube standard (typically ±0.5–1.0% of OD) |
| Straightness | ≤ 1 mm/m (≤ 0.5 mm/m on request) |
| Roundness (ID) | ≤ 50% of ID tolerance |
| Tube ends | Plain, chamfered, or bell-mouthed |
3.2 Materials & Mechanical Properties
| Grade | Equivalent | Yield (min) | Tensile | Elongation (min) |
|---|---|---|---|---|
| E355 (1.0580) | St52 | 355 MPa | 490–630 MPa | 22% |
| E235 (1.0308) | St37 | 235 MPa | 340–480 MPa | 25% |
Also available on request: SAE 1026 DOM (ASTM A513 Type 5), E470 / C45 heavy-duty grades, stainless steel (AISI 304 / 316).
3.3 Popular Sizes (approx. weight at 7.85 g/cm³)
| ID (mm) | OD (mm) | Wall (mm) | Weight (kg/m) |
|---|---|---|---|
| 40 | 50 | 5.0 | 5.5 |
| 50 | 60 | 5.0 | 6.8 |
| 63 | 75 | 6.0 | 10.2 |
| 80 | 95 | 7.5 | 16.2 |
| 100 | 115 | 7.5 | 19.9 |
| 100 | 120 | 10.0 | 27.1 |
| 125 | 145 | 10.0 | 33.3 |
| 160 | 180 | 10.0 | 41.9 |
| 200 | 224 | 12.0 | 62.7 |
Custom OD/ID combinations produced to order.
4. Key Advantages
Work-hardened bore surface — burnishing cold-works the bore, typically raising surface hardness by 10–20% for improved wear resistance and longer seal life
Mirror finish (Ra 0.2–0.4 μm) — smoother than typical honing, reducing seal friction, wear, and scoring
Tight, consistent bore — H8/H9 held along the full length for smooth piston travel
Improved fatigue performance — compressive residual stress in the bore surface layer
One-pass efficiency — shorter production time and better unit cost than multi-pass honing, especially at volume
Ready to use — cut, deburr, weld end fittings, and assemble; no additional finishing required
5. SRB vs. Conventional Honing
| SRB Tube | Honed Tube | |
|---|---|---|
| Process | Skive + burnish, single pass | Multi-pass abrasive honing |
| Bore finish | Ra 0.2–0.4 μm (smooth, dense) | Ra 0.4–0.8 μm (crosshatch) |
| Surface hardness | Increased (cold-worked) | Unchanged |
| Production speed / cost | Faster / lower | Slower / higher |
| Interchangeability | Direct replacement for most cylinder designs | — |
Both processes deliver functionally interchangeable cylinder bores for the majority of hydraulic applications. SRB is the more efficient choice at volume; honing's crosshatch pattern is preferred in certain low-speed, boundary-lubrication designs.
6. Applications
Construction machinery — excavators, wheel loaders, cranes, piling rigs
Agricultural equipment — tractors, harvesters, front loaders, implement cylinders
Trucks & trailers — tipping/dump bodies, refuse collection vehicles
Material handling — forklift masts, scissor lifts, dock levelers
Industrial hydraulics — presses, injection molding machines, machine tools
Mining, marine, offshore & energy — heavy-duty and custom cylinders
7. Quality Assurance
100% eddy-current testing (EN 10246-3); ultrasonic testing for heavy walls on request
Dimensional inspection with bore/air gauges, micrometers, and roughness testers
Mechanical testing: tensile, hardness (surface and body)
Optional hydraulic pressure test
Certification per EN 10204 3.1 with full material traceability
8. Packaging & Delivery
Anti-rust oil on ID and OD; plastic end caps
Bundled with nylon/steel straps, wrapped in plastic film or woven bags; wooden or steel crates for ocean freight
Custom shipping marks, tags, and barcodes available
MOQ: typically 1–2 tons per size (trial orders welcome)
Lead time: typically 15–25 days
9. FAQ
Q: Is SRB tube interchangeable with honed tube?A: Yes. Both deliver H8/H9 bores suitable for hydraulic cylinder barrels, and most customers switch without any design changes. Verify only if your design specifically requires a honed crosshatch.
Q: Can you supply cut-to-length tubes?A: Yes. Cut-to-length with chamfered ends is standard; further machining to your drawing is available on request.
Q: What certificates are supplied?A: EN 10204 3.1 mill test certificates covering chemical composition, mechanical properties, and dimensional inspection.


total 0 Sheet,Only 5 images can be uploaded, each less than 5m.