


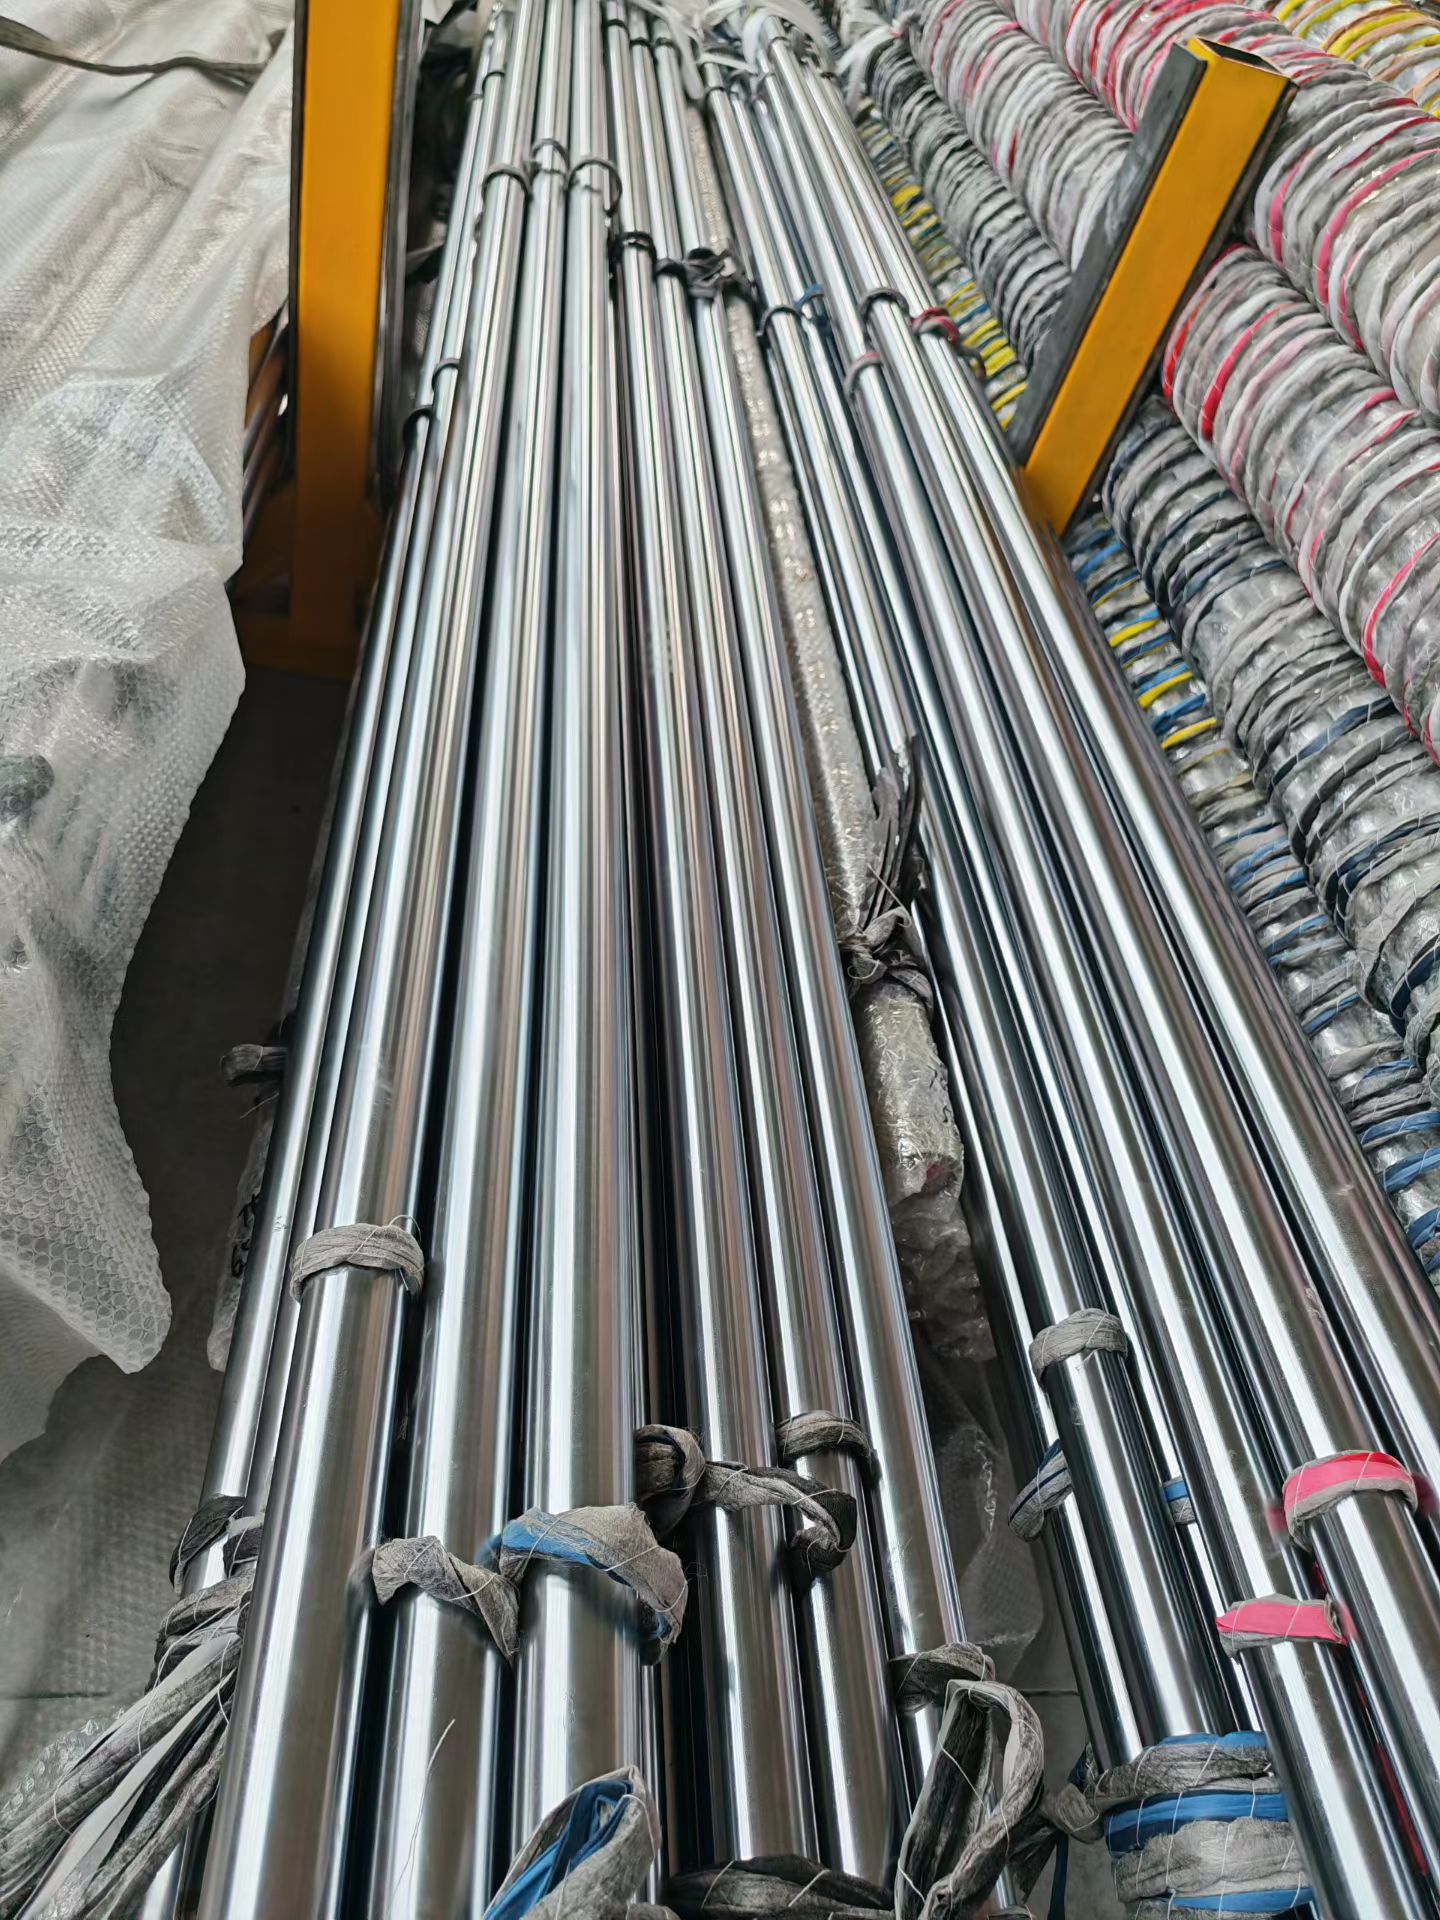
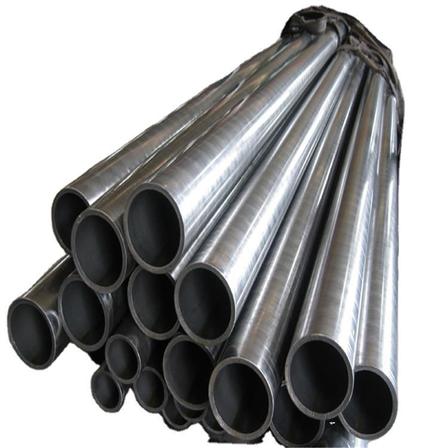
Seamless Honed Steel Tubes
Seamless honed steel tubes are produced from cold-drawn seamless mother tubes and precision-honed on the inner diameter to a mirror-like finish. With tight ID tolerances (H8/H9), low bore roughness (Ra 0.2–0.4 µm) and a uniform cross-hatch pattern for oil retention, our honed tubes are ready for direct hydraulic cylinder assembly — no further boring required.
Product Highlights
Seamless construction — made from seamless steel tube, no weld seam, uniform strength for high-pressure service
Precision-honed bore — ID tolerance to H8/H9 (ISO 286), surface roughness Ra 0.2–0.4 µm
Cross-hatch honing pattern — retains the lubricating oil film, reduces seal wear and extends cylinder life
Wide size range — ID 30–500 mm, OD 40–550 mm, wall thickness 2.5–40 mm
Full material traceability — EN 10204 3.1 mill test certificate, 100% eddy-current tested
Ready to assemble — cut to length, chamfered ends, rust-proofed and capped
Technical Specifications
| Item | Parameter |
|---|---|
| Product Type | Seamless cold-drawn tube, ID honed |
| Outer Diameter (OD) | 40 – 550 mm |
| Inner Diameter (ID) | 30 – 500 mm |
| Wall Thickness | 2.5 – 40 mm |
| ID Tolerance | H8 / H9 (ISO 286); H7 on request |
| OD Tolerance | h9 / h10 |
| ID Surface Roughness | Ra 0.2 – 0.4 µm |
| Straightness | ≤ 0.5 mm/m (tighter on request) |
| Length | 2 – 12 m; cut-to-length available from 500 mm |
| Standards | EN 10305-1 / DIN 2391, ASTM A519, GB/T 3639 |
| End Finish | Chamfered both ends, plastic caps |
| Certificates | EN 10204 3.1 MTC, eddy current test report |
ID Tolerance Reference (ISO 286)
| Nominal ID (mm) | H8 (mm) | H9 (mm) |
|---|---|---|
| > 30 – 50 | +0.039 / 0 | +0.062 / 0 |
| > 50 – 80 | +0.046 / 0 | +0.074 / 0 |
| > 80 – 120 | +0.054 / 0 | +0.087 / 0 |
| > 120 – 180 | +0.063 / 0 | +0.100 / 0 |
| > 180 – 250 | +0.072 / 0 | +0.115 / 0 |
| > 250 – 315 | +0.081 / 0 | +0.130 / 0 |
Popular Sizes (mm)
| ID | OD | Wall | ID | OD | Wall |
|---|---|---|---|---|---|
| 40 | 50 | 5 | 100 | 115 | 7.5 |
| 50 | 60 | 5 | 125 | 145 | 10 |
| 63 | 75 | 6 | 140 | 160 | 10 |
| 80 | 95 | 7.5 | 160 | 180 | 10 |
| 90 | 105 | 7.5 | 180 | 200 | 10 |
Custom ID/OD combinations and non-standard sizes available on request.
Material Grades
| Standard | Grade | Equivalent | Main Application |
|---|---|---|---|
| EN 10305-1 / DIN 2391 | E235 (ST37) | AISI 1020 / 20# | General purpose, low pressure |
| EN 10305-1 / DIN 2391 | E355 (ST52.3) | 16Mn | Standard hydraulic cylinders |
| GB/T 3639 | 45# | AISI 1045 / C45 | Medium-high pressure cylinders |
| GB/T 3077 | 27SiMn | — | High-pressure, heavy-duty cylinders |
| ASTM A519 | 4140 | 42CrMo | High-strength, demanding applications |
Chemical Composition (Typical, %)
| Grade | C | Si | Mn | P ≤ | S ≤ | Cr | Mo |
|---|---|---|---|---|---|---|---|
| E355 (ST52.3) | ≤ 0.22 | ≤ 0.55 | ≤ 1.60 | 0.035 | 0.035 | — | — |
| 45# | 0.42–0.50 | 0.17–0.37 | 0.50–0.80 | 0.035 | 0.035 | — | — |
| 27SiMn | 0.24–0.32 | 1.10–1.40 | 1.10–1.40 | 0.035 | 0.035 | — | — |
| 4140 | 0.38–0.43 | 0.15–0.35 | 0.75–1.00 | 0.040 | 0.040 | 0.80–1.10 | 0.15–0.25 |
Mechanical Properties (Typical)
| Grade | Yield Strength (MPa) | Tensile Strength (MPa) | Elongation (%) |
|---|---|---|---|
| E355 (+N) | ≥ 355 | 470 – 630 | ≥ 22 |
| 45# (N) | ≥ 355 | ≥ 600 | ≥ 16 |
| 27SiMn (Q&T) | ≥ 835 | ≥ 980 | ≥ 12 |
| 4140 (Q&T) | ≥ 655 | ≥ 930 | ≥ 12 |
Exact values depend on delivery condition (+AR / +N / +C / +Q&T) and are stated in the mill test certificate of each batch.
Manufacturing Process
Mother tube selection — hot-rolled or cold-drawn seamless tube, incoming inspection
Cold drawing — precise control of OD and wall thickness
Stress-relief annealing — stabilizes dimensions and removes residual stress
Straightening & cutting — to required length
Precision honing — multi-stone honing head produces the specified cross-hatch finish and ID tolerance
Cleaning & drying — bore flushed, dried and inspected
Final inspection — dimensions, roughness, straightness, eddy current testing
Oiling & capping — rust-preventive oil applied, ends capped and packed
Skive & roller burnishing (SRB) available as a faster alternative process for high-volume orders.
Applications
Hydraulic cylinder barrels for excavators, loaders, cranes, dump trucks
Telescopic cylinders for tippers and trailers
Agricultural and forestry machinery
Mining and tunneling equipment
Industrial hydraulics: presses, injection molding machines, machine tools
Material handling: forklifts, aerial work platforms
Pneumatic cylinders and general precision tubing
Quality Assurance
100% eddy current testing (EN 10305-1 / DIN 2391-2)
Hydrostatic pressure testing and UT testing on request
Full dimensional and surface roughness inspection with calibrated instruments
ISO 9001 certified quality management system
Batch traceability from mother tube to finished product
Packing & Delivery
Bore coated with rust-preventive oil, both ends sealed with plastic caps
Each tube wrapped in PE film; bundles packed in steel crates or on steel pallets
Wooden cases for cut-to-length pieces
Sea-worthy export packaging; container loading plan provided


total 0 Sheet,Only 5 images can be uploaded, each less than 5m.