

ST52 Honed Tube
ST52 honed tube is a cold-drawn seamless precision steel tube whose inner bore has been finish-machined by honing to achieve tight dimensional tolerances and an exceptionally smooth, low-friction surface. The ST52 designation refers to a low-carbon manganese steel with a minimum yield strength of 355 MPa (520 MPa in some cold-finished conditions), and it is the material grade most widely specified for hydraulic cylinder barrels under the legacy DIN 2391 standard and its current European equivalent, EN 10305-2 (grade E355 / 1.0580).
The honed bore allows the tube to serve directly as a cylinder barrel in hydraulic and pneumatic systems, eliminating the need for secondary boring or reaming before assembly. The result is a ready-to-machine component with a uniform, cross-hatched surface texture that promotes oil retention, stable piston sealing, and consistent pressure transmission over long service intervals.
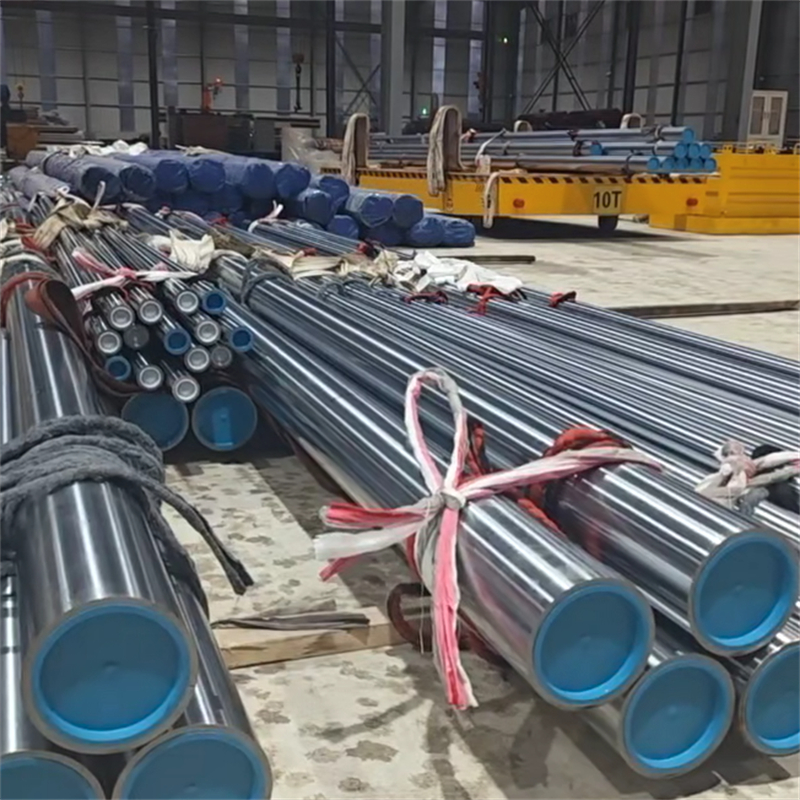
Material & Standards
| Item | Specification |
|---|---|
| Material grade | ST52 / ST52.3 / E355 / 1.0580 |
| Standard | DIN 2391, EN 10305-2, EN 10305-1 |
| Delivery condition | BK+S (cold drawn, stress relieved), +N (normalized) |
| Manufacturing route | Cold-drawn seamless → stress relief → honing / SRB |
ST52 is the German designation; E355 is the EN designation for the same low-carbon manganese steel family. Both are interchangeable for most hydraulic cylinder applications, and material certificates can be issued to EN 10204 3.1 upon request.
Chemical Composition (Typical, wt. %)
| Element | C | Mn | Si | P (max) | S (max) |
|---|---|---|---|---|---|
| ST52 / E355 | ≤ 0.22 | ≤ 1.60 | ≤ 0.55 | 0.025 | 0.025 |
The low carbon and controlled manganese range give ST52 a balanced combination of strength, weldability, and machinability, while the restricted phosphorus and sulfur levels support consistent honing response and surface integrity.
Mechanical Properties
| Property | Typical Value |
|---|---|
| Yield strength (Rₑ, min.) | 355 MPa (base grade); 470–520 MPa achievable in cold-drawn + stress-relieved condition |
| Tensile strength (Rₘ) | 490–640 MPa |
| Elongation (A, min.) | ≥ 15–22% depending on condition and direction |
| Hardness | Approx. 180–220 HB (varies with wall thickness and delivery condition) |
Cold drawing and stress relieving raise the yield strength well above the 355 MPa base level, which is why ST52 honed tube is routinely used in cylinders operating at high working pressures.
Key Dimensional & Surface Specifications
| Parameter | Standard Range | Precision Capability |
|---|---|---|
| Inside diameter (ID) | 40 – 500 mm | up to 1,000 mm on request |
| Outside diameter (OD) | 50 – 600 mm | — |
| Wall thickness | 3 – 50 mm | up to 80 mm special |
| ID tolerance | H8 / H9 | H7 available |
| ID surface roughness (Ra) | Ra ≤ 0.4 – 0.8 µm (honed) | Ra ≤ 0.2 – 0.4 µm (SRB / precision honed) |
| Straightness | ≤ 1 mm/m | ≤ 0.3 mm/m available |
| Standard length | 3 – 9 m | up to 12–13 m on request |
| Tube ends | Square cut, burr-free, plastic caps | Chamfered / threaded on request |
H8 is the default bore tolerance for cylinder barrels under ISO 286-2; H7 and H9 are available where the cylinder design requires a tighter or more open fit. The honed cross-hatch pattern is deliberately retained rather than fully polished, because the fine grooves help maintain an oil film between the piston seal and the bore wall.
Core Advantages
Ready-to-assemble bore. Honing brings the ID directly to H8/H9 tolerance and Ra 0.4 µm or better, so the tube can go straight to cylinder assembly without a separate boring operation.
Seamless integrity. Produced from a solid billet and cold-drawn without a weld seam, the tube offers uniform circumferential strength and avoids weld-line discontinuities that can act as leak paths or fatigue initiation sites in pressure-cycled cylinders.
Low friction, stable sealing. The controlled surface topography reduces piston seal friction and wear, helping maintain repeatable cylinder response and extending seal life in high-cycle applications.
Material consistency. ST52/E355 is a well-characterized low-carbon manganese steel with predictable response to honing, welding, and machining, making it a low-risk choice for both OEM production and MRO replacement barrels.
Flexible sizing and delivery condition. ID from 40 mm to 500 mm as standard, lengths to 12–13 m, with BK+S or +N delivery conditions and custom cutting to drawing.
Typical Applications
ST52 honed tube is specified primarily where a smooth, dimensionally stable bore is required for a sliding seal or piston:
Hydraulic cylinder barrels — construction machinery (excavators, loaders, cranes, bulldozers), hydraulic presses, injection molding machines
Pneumatic cylinders — general automation and material handling
Telescopic and servo cylinders — where bore roundness and straightness directly affect rod guidance and seal performance
Agricultural equipment — tractor implement circuits, harvesters, sprayers
Material handling — forklift mast and tilt cylinders, aerial work platforms
General engineering — bushings, guide tubes, and fluid-transfer components requiring a precision bore
Manufacturing & Quality Control
The production route is controlled at each step from strip/solid billet to finished honed tube:
Cold drawing — seamless tube reduced to near-final OD and ID.
Stress relief — BK+S condition applied to stabilize dimensions and relieve drawing stresses.
Honing — abrasive stones remove a controlled layer from the ID, correcting roundness, straightness, and size while generating the cross-hatch finish.
Inspection — ID/OD measured with bore gauges and micrometers; surface roughness checked with profilometer; straightness verified on surface plates or laser equipment.
Protection — anti-rust oil applied internally and externally, ends capped, bundled with steel strips.
Typical inspection reports cover chemical composition, tensile properties, ID tolerance, wall thickness, straightness, and surface roughness. Third-party inspection (SGS, BV, or equivalent) can be arranged.
Packing & Delivery
Packing: anti-rust oil on ID and OD, plastic caps on both ends, steel-strip bundles, braided wrap or wooden crates for export.
Length tolerance: +2 mm for lengths ≤ 500 mm; +3 mm for 500–2,000 mm; +5 mm for 2,000–5,000 mm; +10 mm for > 5,000 mm.
Lead time: typically 20–30 days after order confirmation, depending on size and quantity.
FAQ
Q: Is ST52 the same as E355?
Yes, for honed cylinder tube purposes ST52 (DIN 2391) and E355 (EN 10305-2) are treated as equivalent grades. The chemical composition and mechanical property requirements overlap, and material can be certified to either designation.
Q: What is the difference between honed and SRB tube?
Honing uses abrasive stones to correct geometry and generate the cross-hatch finish. SRB (skived and roller burnished) is a single-pass alternative that can achieve lower roughness (Ra ≤ 0.2–0.4 µm) at higher production speeds and introduces a cold-worked surface layer. Both are available depending on bore size, quantity, and surface requirement.
Q: Can you supply H7 tolerance?
Yes. H8 is standard for cylinder barrels, but H7 can be produced on request for applications requiring a tighter bore fit.
Q: What is the maximum length?
Standard supply is 3–9 m. Lengths up to 12–13 m are available for large-diameter or special project orders.
Q: Do you provide material certificates?
Yes. EN 10204 3.1 mill certificates are available, and third-party inspection can be arranged before shipment.


total 0 Sheet,Only 5 images can be uploaded, each less than 5m.